
Improving Productivity and Decreasing Costs
CLIENT INDUSTRY: Packaging Manufacturer
SOLUTION: Operational Excellence, Supply Chain
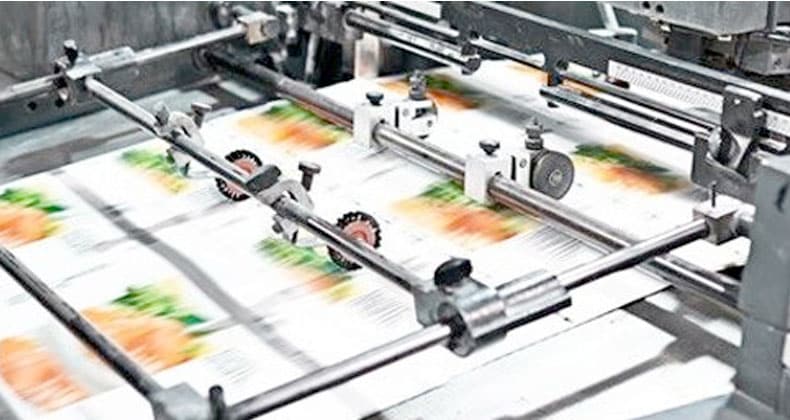
Our client produced labels for consumer goods and food products. The company lacked the capacity to meet its customers’ volume and variety requirements. This demand was met with additional shifts and selective outsourcing.
The recent loss of large client orders and contractual penalties for late deliveries made, the company stood to lose money and orders if it could not meet promised delivery dates.
Business Challenge
The company needed to increase capacity without a large capital equipment investment. Greatly reducing the non-value added (NVA) time in the production process could provide the needed production capacity. One source of NVA time was relatively long changeover and setup times (in some cases more than three hours).
Solution
- CBS led a Kaizen event to analyze and improve the process
- A team of employees was assembled. CBS trained the team on Lean Production tools, specifically, SMED – Single Minute Exchange of Dies and other quick setup/changeover techniques.
- The team then observed several changeovers or “make readies.” All related process steps were listed and categorized as:
- Value-add (VA) vs. Non-value add (NVA)
- Internal (machine is running) or External (machine not running) events
- The RCE team analyzed all of the data collected and formulated several recommendations. Once piloted, the team developed a final recommendation, and they developed a set of Make Ready procedures to support the recommendation
Results
- The resulting recommendations reduce the average changeover by 60% – from 100 minutes to 39 minutes
- The workforce was empowered to make informed decisions regarding their work areas and procedures
- Enabled the plant to reduce weekend shifts and reduce the need for temporary workers
- Cost avoidance of adding another press ($300 – 500K)
Latest Insights
-
The Headcount Band-Aid: When more people won’t fix the problem
When output slips, most companies hire, because headcount is visible and processes are not. Brad Crnich breaks down what the headcount band-aid actually costs:…
-
Why Multi-Site Manufacturing Operations Lose Execution Control as They Scale
The same operational problems at every plant rarely mean plant problems. Tim Christlieb explains the execution architecture multi-site industrial companies need: consistent planning logic,…
Sign up to receive our latest insights!
"*" indicates required fields